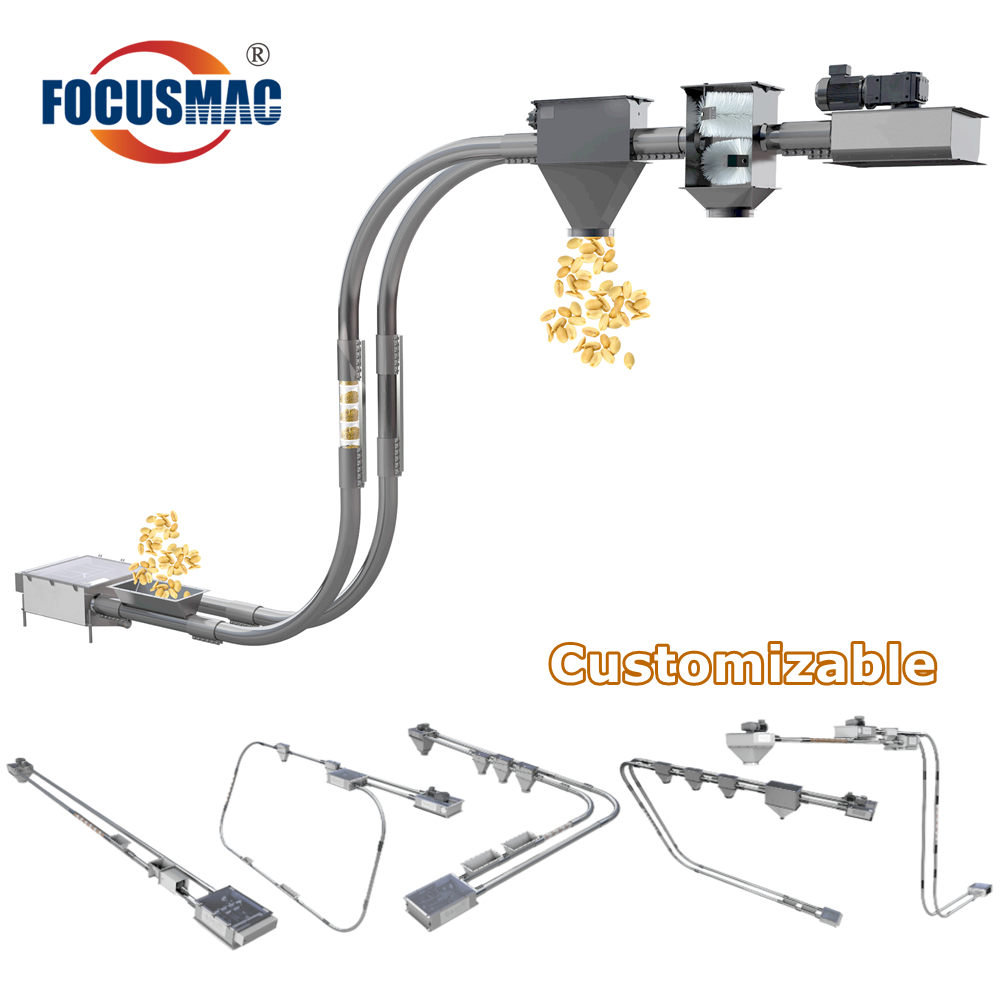
Coffee Beans Rubber Chain Bucket Elevator
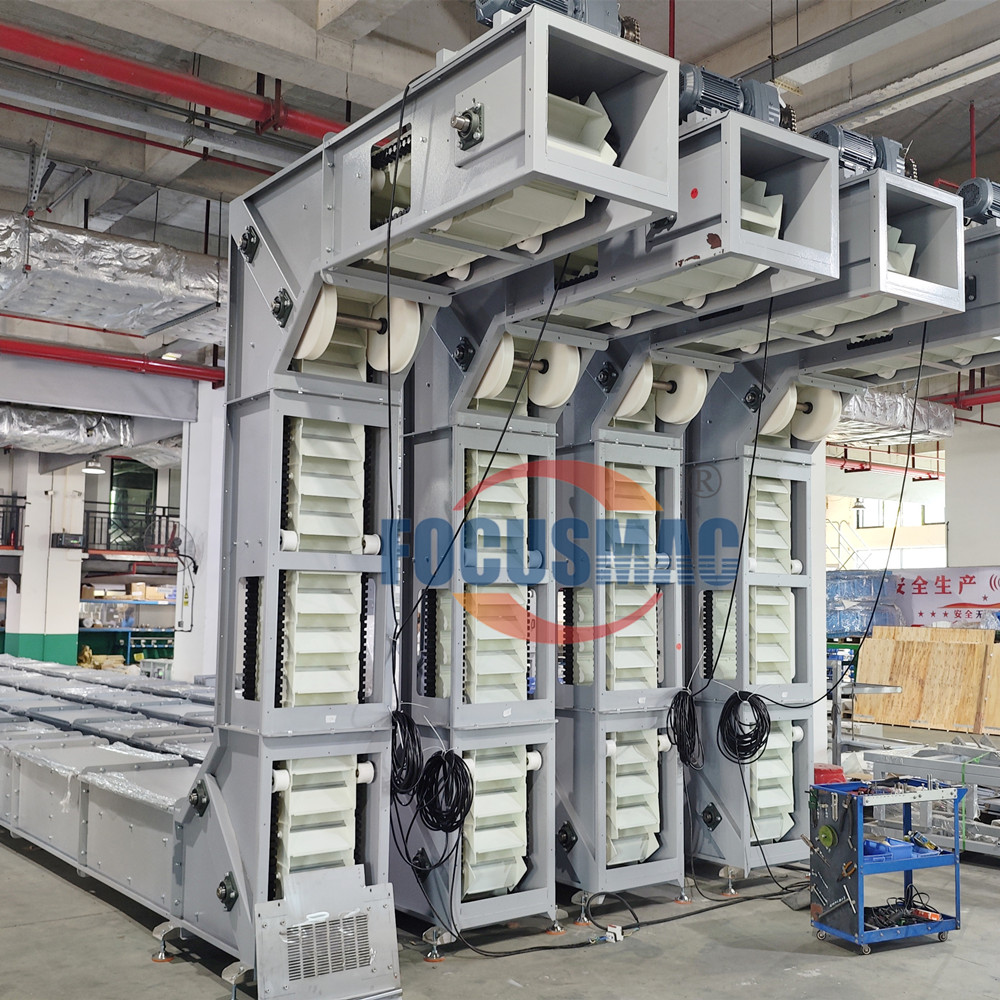
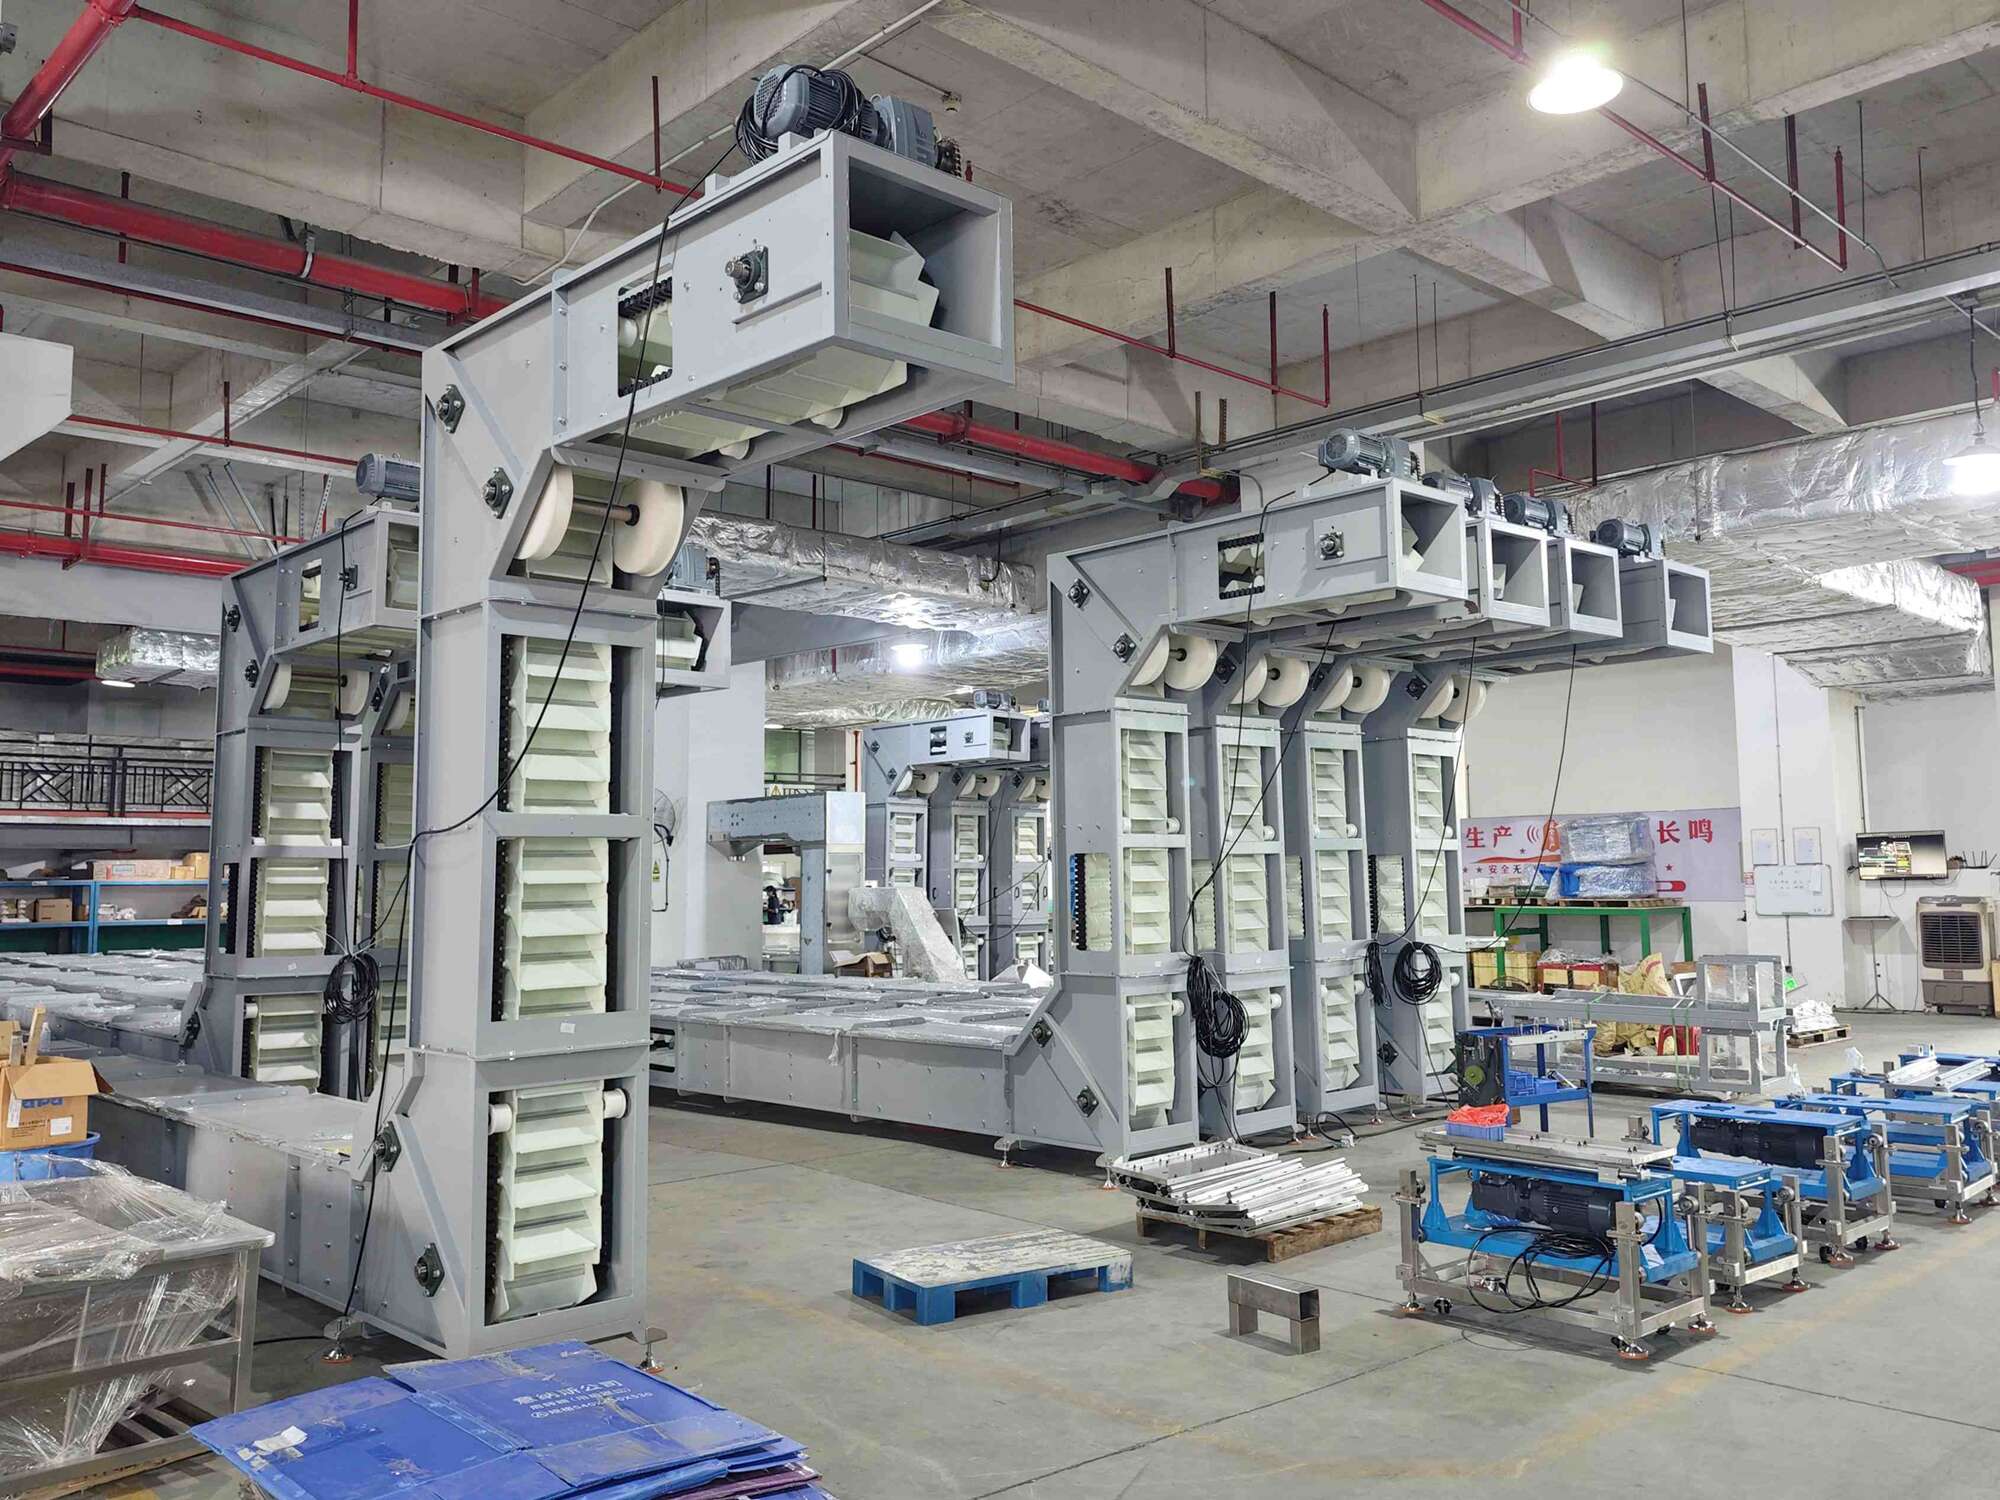
This new design rubber chain bucket elevators feature a rubber chain system that make them cleaner, quieter, and more reliable than conventional metal chain elevators.Capable of running in extremely harsh and dusty environments, the systems are also vibration-free, abrasion-proof.
Rubber Chain Bucket Elevator
This new design bucket elevators feature a rubber chain system that make them cleaner, quieter, and more reliable than conventional metal chain elevators.Capable of running in extremely harsh and dusty environments, the systems are also vibration-free, abrasion-proof.
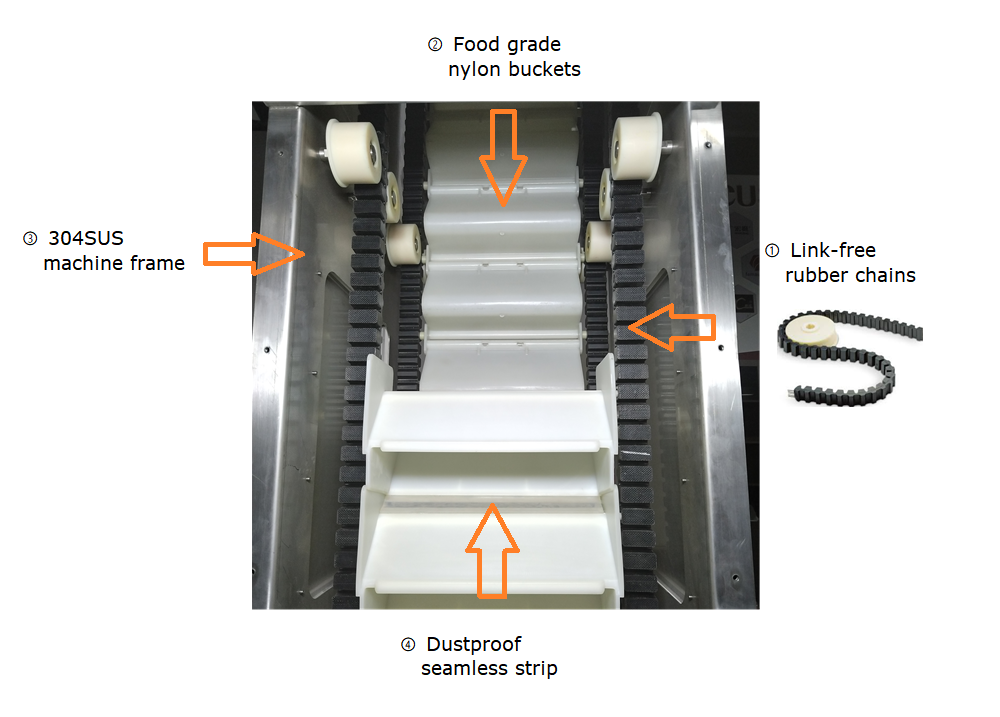
Features of Rubber Chain Bucket Elevator:
Iron-chain bucket elevators generate metal wear powder that contaminates product, corrode under harsh conditions, and never run quietly. This continuous rubber chain bucket elevator eliminates every one of those failure points for plants where contamination and downtime are not acceptable.
1. Rubber Chain with 3 to 10 Embedded Steel Wires:
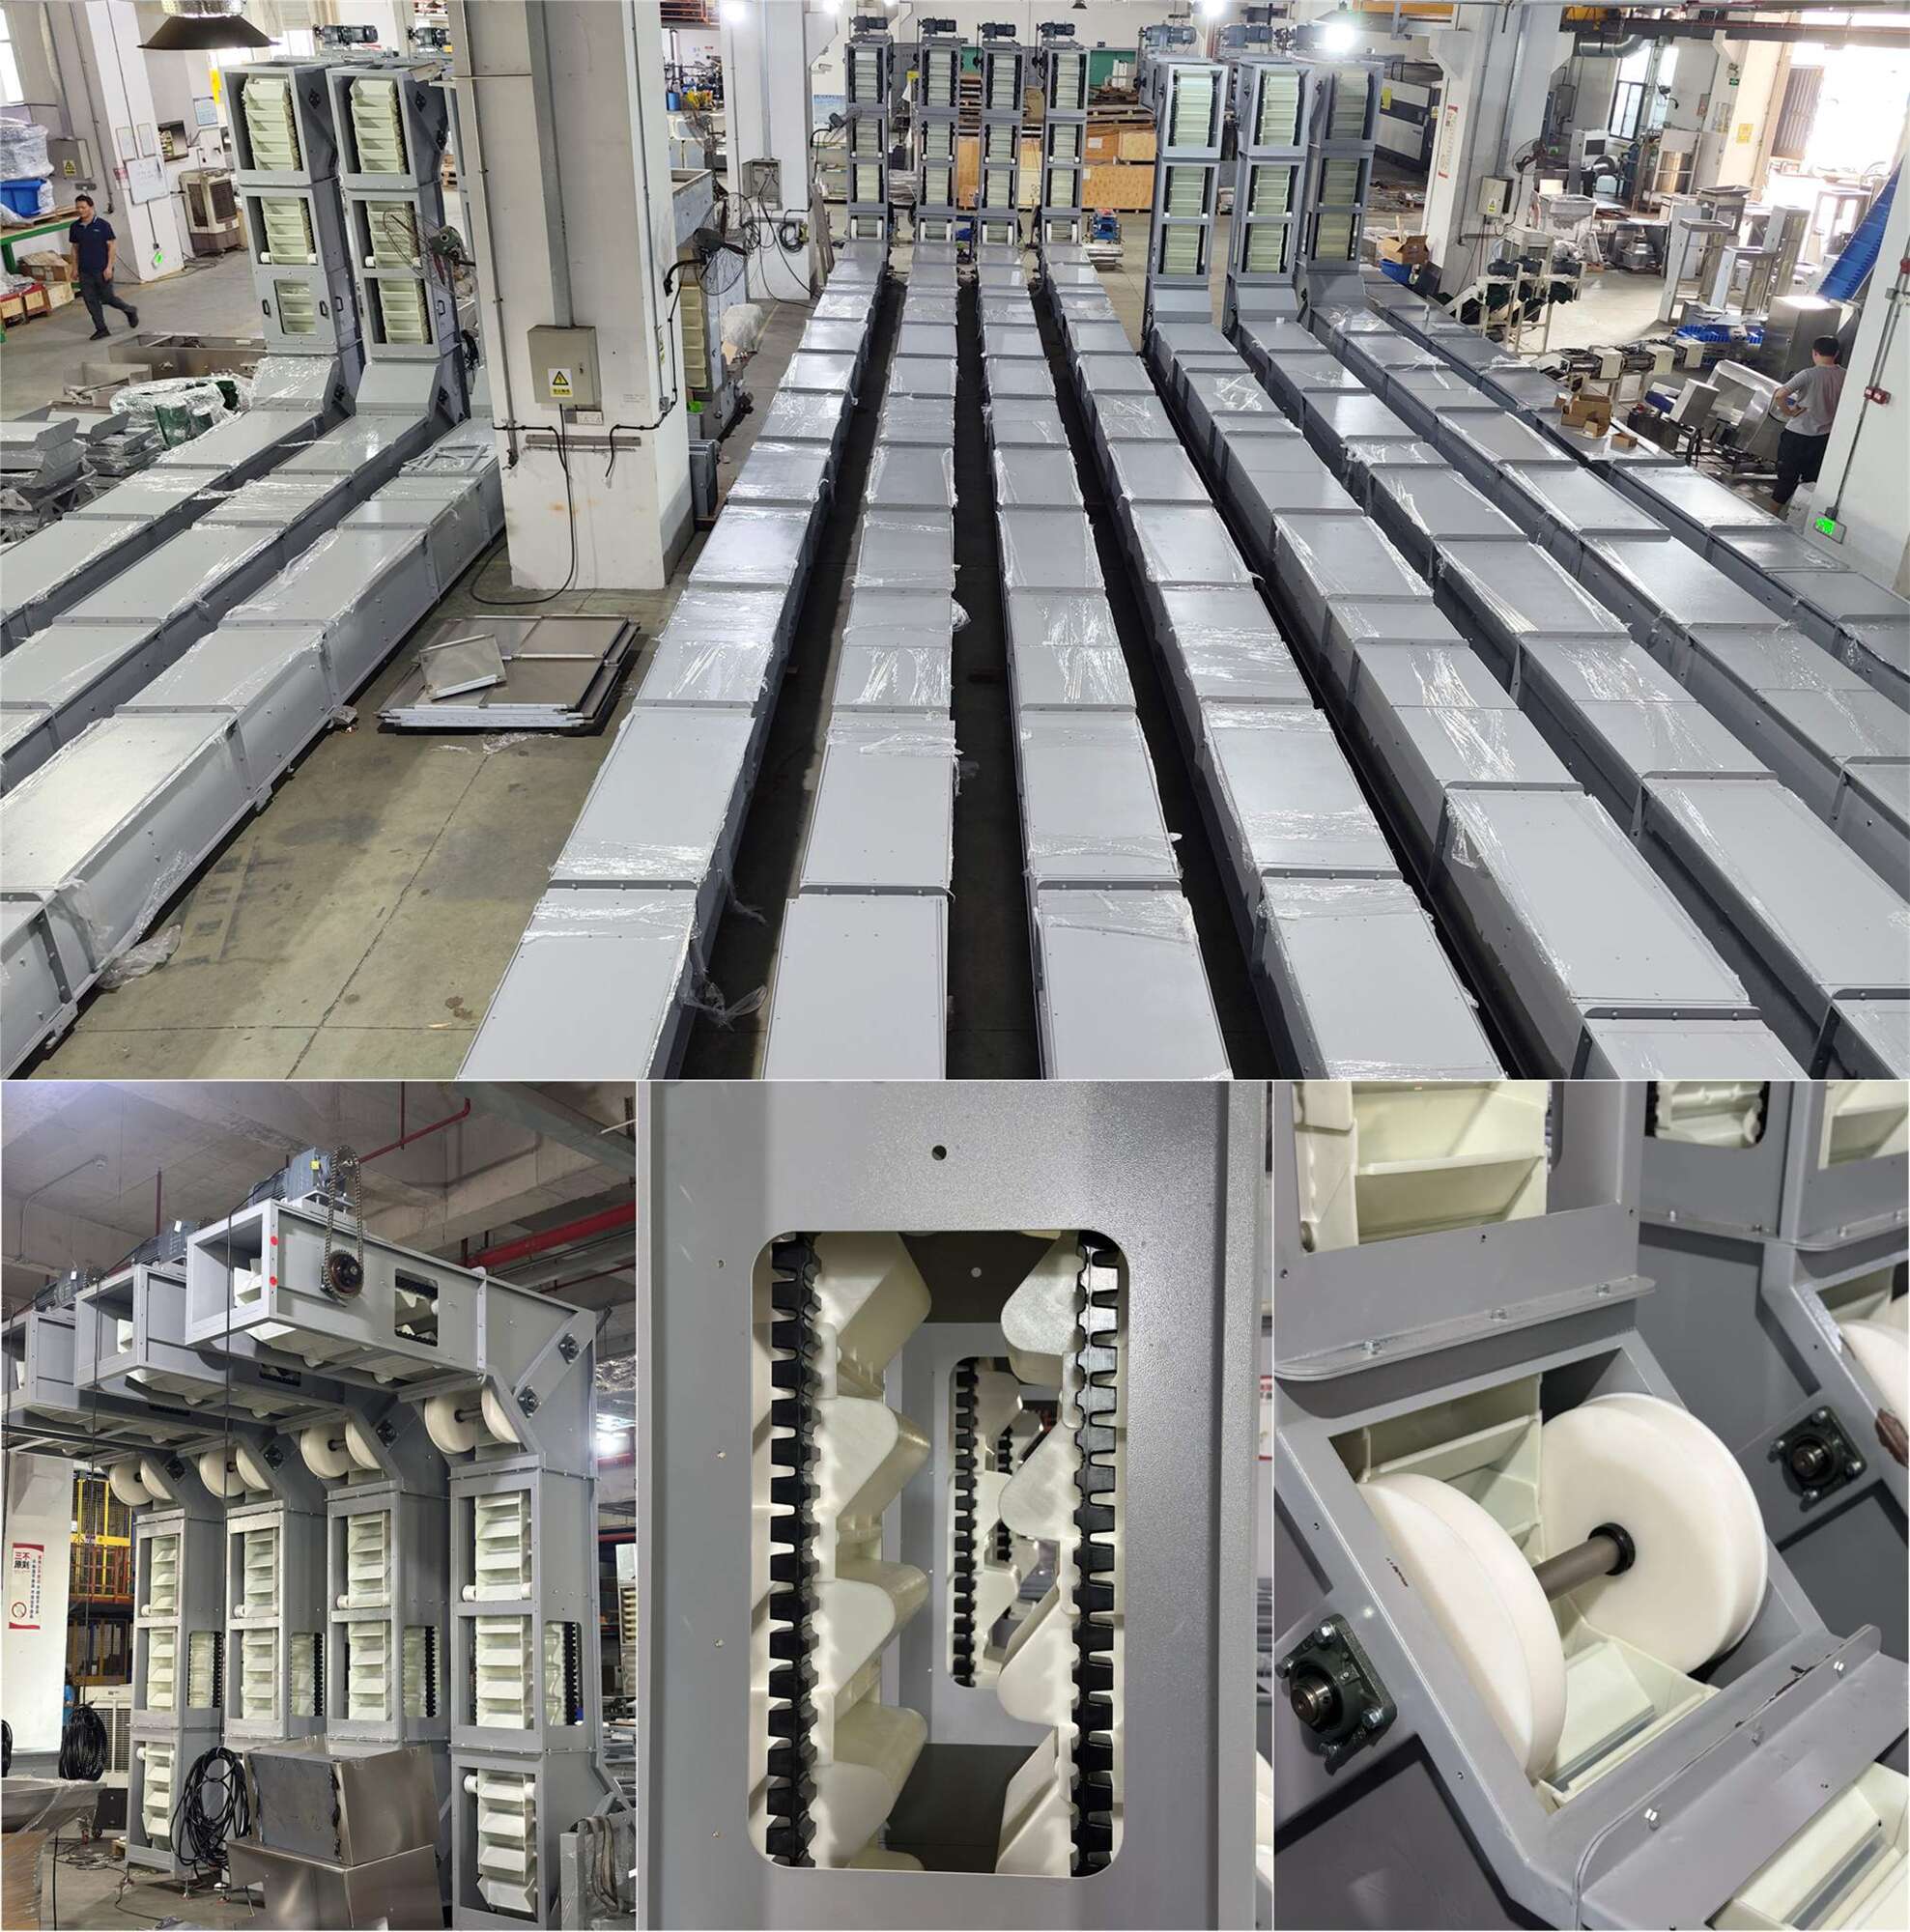
The drive chain is a solid rubber body with steel wire cords vulcanised into the core, combining iron-chain tensile strength with rubber elasticity. Zero metal-on-metal contact means zero wear powder and zero product contamination. No lubrication needed, no rust, and significantly longer service life than conventional iron chains.
2. Nylon Buckets with Rubber Sealing Strips Between Every Bucket:
High-strength nylon buckets are lightweight, impact-resistant, and corrosion-resistant. Rubber sealing strips close every gap between adjacent buckets, preventing dust infiltration, stopping material spillage, and eliminating dropped-bucket failures common in iron-chain elevators.
3. Up to 30 Cubic Metres Per Hour, Up to 20 Metres Lift Height:
Continuous operation with no pulsing or surging delivers up to 30 cubic metres per hour. Maximum lift height reaches 20 metres. Both capacity and height are customisable to your project requirements.
4. Explosion-Proof, Corrosion-Resistant and Dust-Proof:
Rated explosion-proof for chemical powder, grain dust, and battery material environments. Fully corrosion-resistant for salt and acid conditions. Sealed casing and bucket-to-bucket rubber strips lock contamination out through the full lift cycle.
5. Silent Operation:
Rubber chain on polymer guides produces no metal clanking, no chain slap, and no vibration noise.
Technical Parameters:
| Model | Rubber Chain Bucket Elevator |
| Bucket Volume | 3.7L |
| Machine Structure | Stainless steel or carbon steel |
| Production Capacity | 10-30 m3/h |
| Machine Height | Customized |
| Discharging Height | Customzied |
| Hopper Material | Food grade ABS |
| Voltage | AC220V or three phase 380V, 50hz/60hz |
| Power Supply | 0.75kw |
In food industry
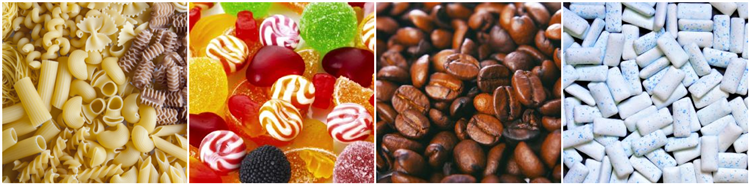
Particularly in the food industry, the advantages of continuous bucket conveyors and pendulum bucket conveyors are clear to see. By using original rubber chains, no lubricants are required that could contaminate the conveyed materials.
The casing can be designed in accordance with the highest hygienic requirements, such as with a tubular framework without horizontal surfaces and dead spaces.
On the pendulum bucket conveyors, the buckets can be removed without tools in a single action to clean them externally. Automatic cleaning stations can also be supplied for cleaning the buckets in all series.
Detectable buckets offer the ability to increase your product safety.
In non-food industry
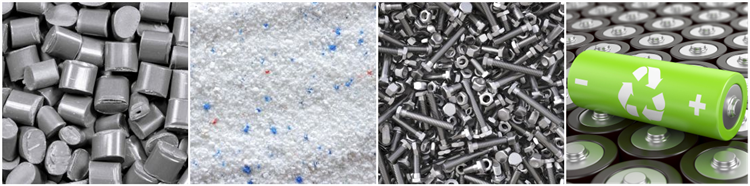
With link-free original rubber chains, continuous bucket and pendulum bucket conveyors have proven themselves in the food and non-food area. Even abrasive materials and those causing wear can be conveyed with ease.
þ Powders and granulates þ Chemicals þ Building materials þ Recycling
þ Ceramics þ Plastics þ Lithium battery þ Non-ferrous metal þ Semiconductor materials
The advantages of rubber chain bucket elevator
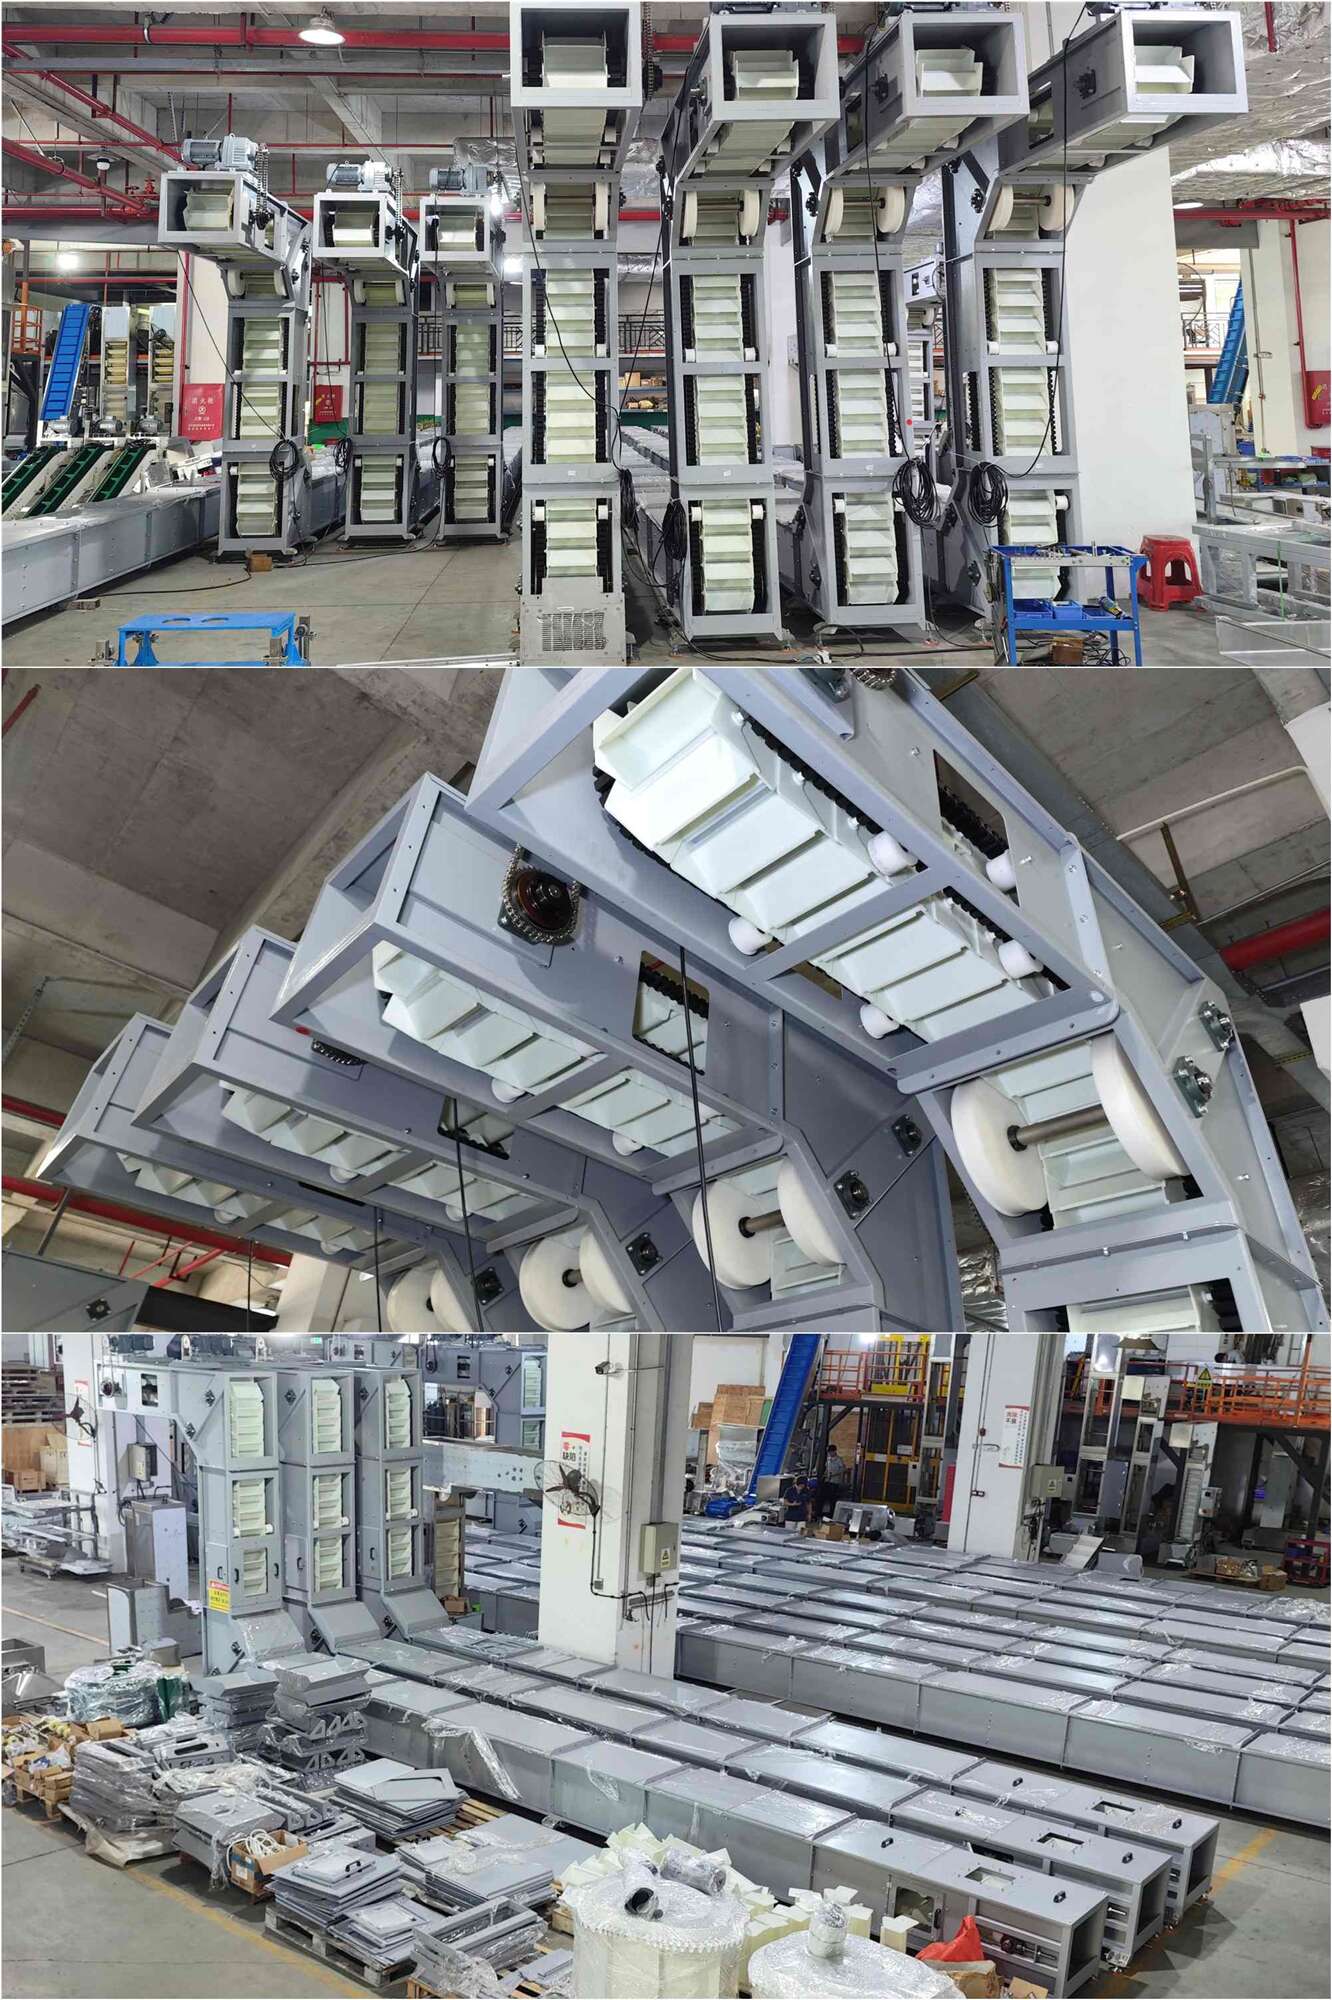
Real shots